

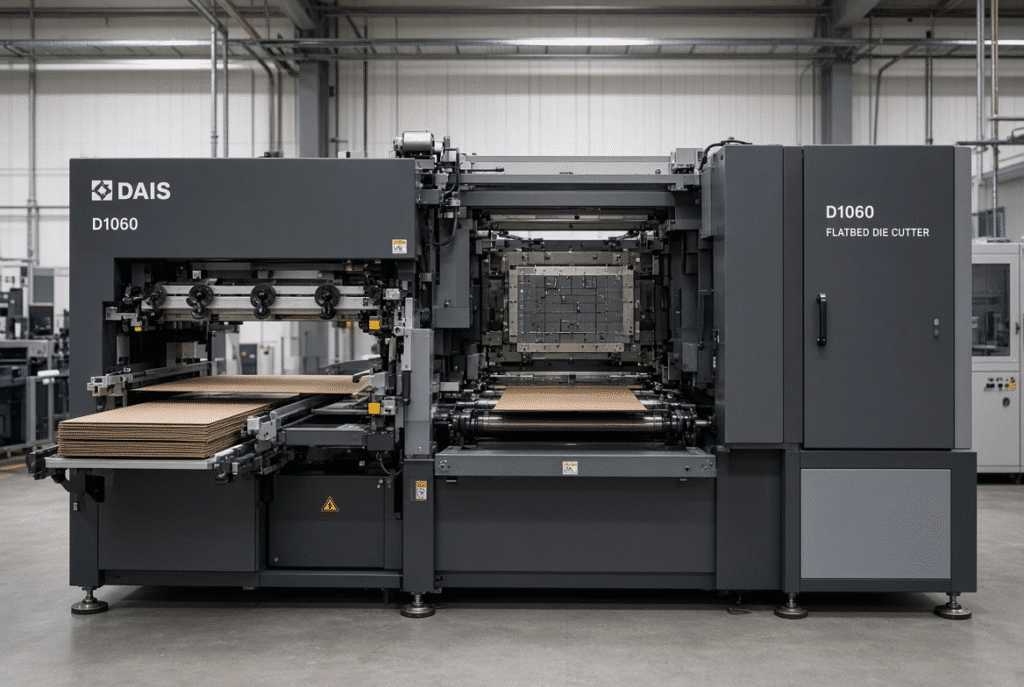
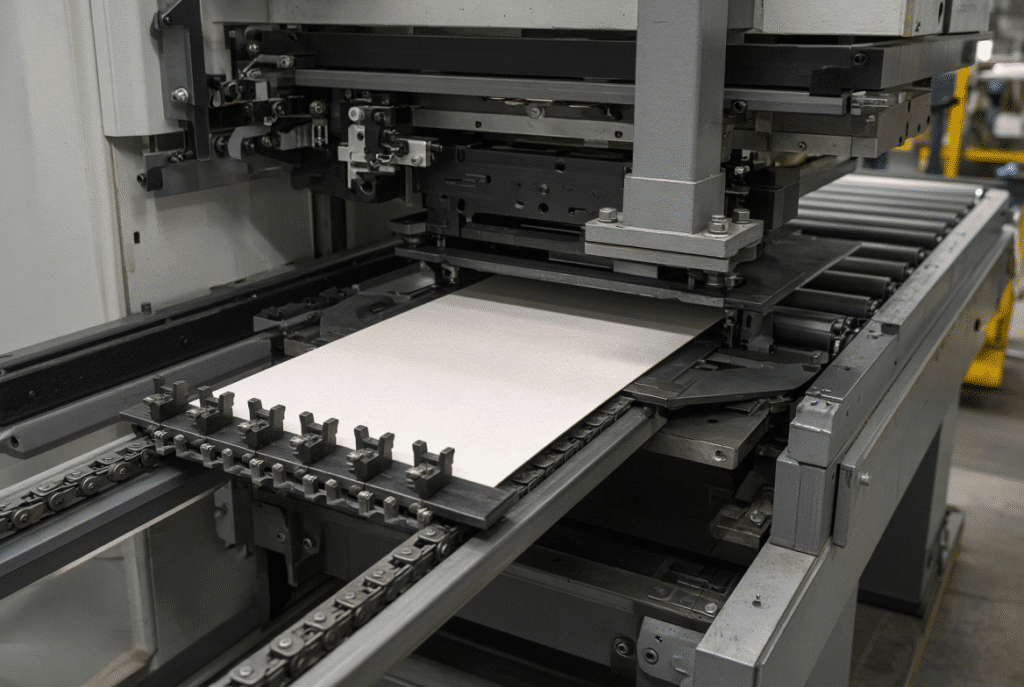
In flatbed die cutters, the sheet transfer system is controlled by an intermittent mechanism, which moves the sheet at a controlled speed to allow the gripper bars to advance, slow down, position and hold the sheet to apply pressure to it by the platen. The mechanism is located between the main drive that is constantly turning and the stop and go drive force needed by the gripper bars and chain. The common symptoms of a worn mechanism, poor lubrication and out-of-adjustment are registration shifts, increasing vibration throughout the range of travel, abnormal noises upon release and start up, and late sheets or bouncing at delivery. When a machine operates quietly at low speed and then produces timing scatter and/or vibrations at production speed, it is a classic warning that the intermittent drive or components associated with it are in need of attention.
What Is an Intermittent Mechanism?
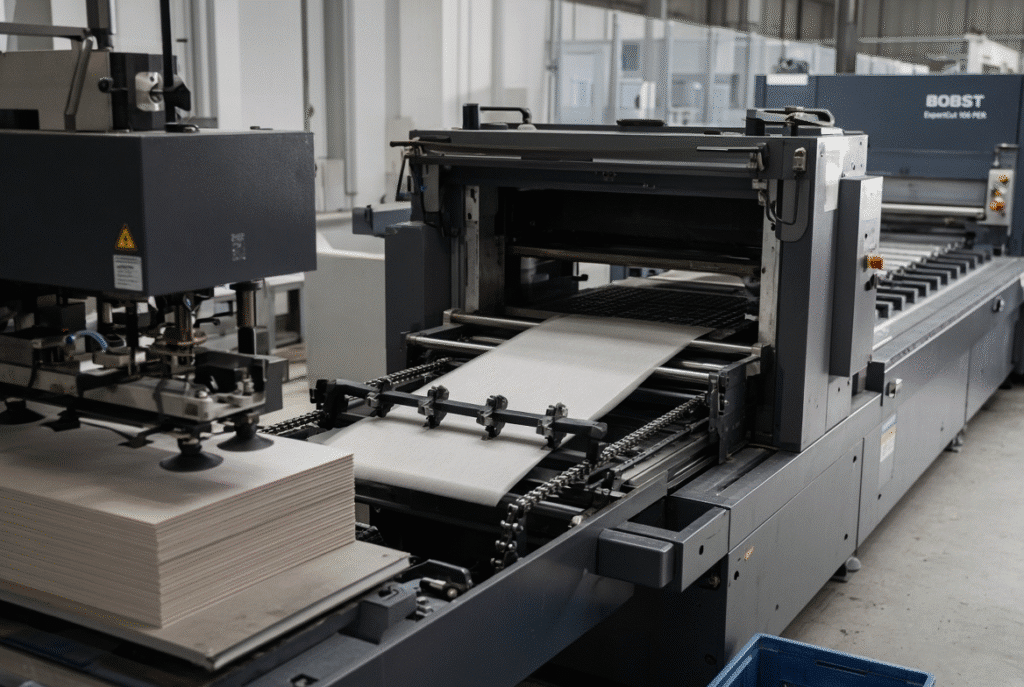
An intermittent mechanism is a mechanism that is used to transmit controlled motion and pause in a periodic manner from the steady motion of the main motor and drive shaft. As the upper platen moves downwards in a platen die cutter, the sheets will not move continuously; they have to stand still or stop while the cutter and die cuts and creates the design. That same intermittent pattern is provided by the intermittent mechanism so the transport system can move, slow down, stop, and get ready for the next cycle without having to make the motor start and stop.
Continuous Rotation Versus Intermittent Movement
The primary drive remains at a fairly constant speed. The gripper-bar and chain system, however, has to move in steps, which follow the die-cutting cycle. The intermittent mechanism is the necessary link between that. It does not stop the motor, but it does control the way the motion is transferred to the transport shafts, sprockets and chains so that eventually, each sheet gets to the right station at the right time, and it is always in control when pressure is applied.
Movement, Deceleration, Dwell and Acceleration
There are four connected phases of a typical transfer cycle. Acceleration is used to get gripper bars and chain moving at transport speed. The board is moved from station to station by sheet transport. Deceleration will allow the system to run at a slower rate which will prevent the sheet from overshooting or hitting the gauges. The sheet is held in place during the closing platen and cutting when the dwell is used (or a controlled low speed positioning period). Once opened, the system will accelerate again for the next transfer. These changes are smooth, which helps to maintain low dynamic loads and repeatable sheet position. Sudden changes create impact on chains, bearings and gripper bars and can lead to registration scatter.
Relationship to Gripper Bars and Chains
The system is driven or timed by the intermittent mechanism, which includes a chain and a gripper-bar. Even if the bottom end of the mechanism is still within tolerance, the damage to the sprocket, the wear or the stretch in the chain will be evident in the form of transfer problems. Similarly, an intermittent drive that is worn will impart the same type of motion irregularity into an otherwise quality chain and gripper. The two should be checked in conjunction.
How Sheet Transfer and Die-Cutting Timing Work Together
Sheet movement through a flatbed die cutter is a continuous sequence of timed events. The intermittent mechanism keeps each event locked to the platen cycle so the sheet reaches the die-cutting position on time and stays under control while pressure is applied.
Feeding and Initial Sheet Capture
The feeder presents the sheet to the gripper bars or entry transport. Timing must allow the grippers to close on a stable, square sheet without collision or delay. If the intermittent drive is late or early, the sheet may slip, skew, or double-feed. The same symptoms can also come from feeder adjustment, sheet curl or sensor misalignment, so the complete entry system should be checked before the intermittent mechanism is assumed to be at fault.
Transfer Into the Die-Cutting Area
Once gripped, the bars accelerate, travel and decelerate so the sheet arrives at the front and side gauges with minimal residual motion. Unstable transfer produces variation in arrival position from sheet to sheet. That variation shows up as print-to-die registration drift, especially on tight layouts or at higher speeds.
Dwell During Die Cutting
The sheet should be stable enough during the dwell or positioning phase so that the platen can exert the full pressure without moving the board. Final registration also relies on the gauge condition, gripper bite, die setup, sheet flatness and overall machine alignment along with the intermittent mechanism creating a required timing window. The mechanism does not ensure accuracy in registering.
Transfer to the Delivery Section
Once the platen has opened, the gripper bars will move the cut sheet towards the delivery point and release it there. The delivery pile can get misaligned, damaged at the edges, or intermittent jams can occur because of late or early release, residual vibration or uneven deceleration. If a machine cuts cleanly but does not give even stacks, then it is likely that there is a time or motion issue in the final transfer phase.
Why Intermittent Mechanism Design Affects Machine Performance
The quality of the motion achieved by the intermittent mechanism will directly affect the way that the rest of the machine will perform under production load.
Motion Smoothness and Mechanical Load
Rapid start/stop loading increases peak forces on chains, sprockets, bearings, gripper bars and the mechanism. Those forces are distributed over a greater percentage of the cycle when the cam or drive is smoother, and this helps to keep the transport system quieter and more consistent.
Timing Repeatability and Registration
Any slight difference in gripper bar arrival time or location is reflected as a change in sheet location at the die. With challenging work those variations appear as obvious registration errors. The repeatability is therefore crucial, but it is not the only one and comes along with material quality, gauges, grippers and condition of the sensors and dies.
Operating Speed and Stability
At low speed many worn or poorly lubricated mechanisms still function acceptably. As speed rises, dynamic forces increase and small clearances, worn surfaces or lubrication gaps begin to produce vibration, noise or timing scatter. Operators often reduce speed to regain control; the underlying mechanical condition has not improved.
Serviceability and Maintenance Access
A well-designed intermittent mechanism still requires regular inspection, lubrication and eventual parts replacement. Buyers should confirm that lubrication points are reachable, that wear components can be obtained, and that the supplier provides clear maintenance diagrams and timing procedures. Accessibility affects real-world uptime as much as the original design quality.
Common Wear Symptoms in Intermittent Mechanisms
Symptoms rarely point to a single cause. The list below links common observations to possible mechanical conditions while stressing that a full system check is always required.
Abnormal Noise During Acceleration or Deceleration
Knocking, clicking, grinding or rattling that appears only when the transport starts or stops often indicates wear in cams, gears, bearings, or loose fasteners. Record the exact phase of the cycle in which the noise occurs and stop the machine for qualified inspection if the sound is new or increasing.
Vibration at Production Speed
Vibration that grows with speed may come from uneven motion, worn bearings, chain elongation, misalignment or mechanical looseness. Compare the behavior at a safe lower speed and note whether the vibration is strongest during acceleration, dwell or delivery transfer.
Registration Drift or Inconsistent Sheet Position
Timing variation can shift the sheet’s arrival position, yet the same symptom can also originate from gauges, gripper condition, sheet quality, sensor alignment or die setup. Do not replace the intermittent mechanism until the complete transport path has been examined.
Jerky or Incomplete Sheet Transfer
Sheets that hesitate, shift sideways, slip in the grippers or arrive late usually indicate a combination of mechanism wear, chain or sprocket problems, gripper issues, contamination or incorrect setup. Systematic diagnosis is more effective than random adjustments.
Increased Heat or Lubricant Consumption
Excessive friction, oil or grease leakage, or oil and grease misalignment may be indicated by unusual heat or an increase in oil and grease usage. Do not use absolute temperatures, use the current readings against a baseline that represents the machine’s normal state.
Repeated Machine Stops or Cycle Alarms
Modern controls prevent the machine from operating if the timing, position or safety signals are outside of the approved range. A mechanical, electrical, sensor or pneumatic failure of some kind could be the root cause. Just resetting the alarms is not the real diagnosis; it is merely postponement.
Maintenance Practices for Intermittent Mechanisms
Operator and technician level work should be distinctly different.
Cleaning and Contamination Control
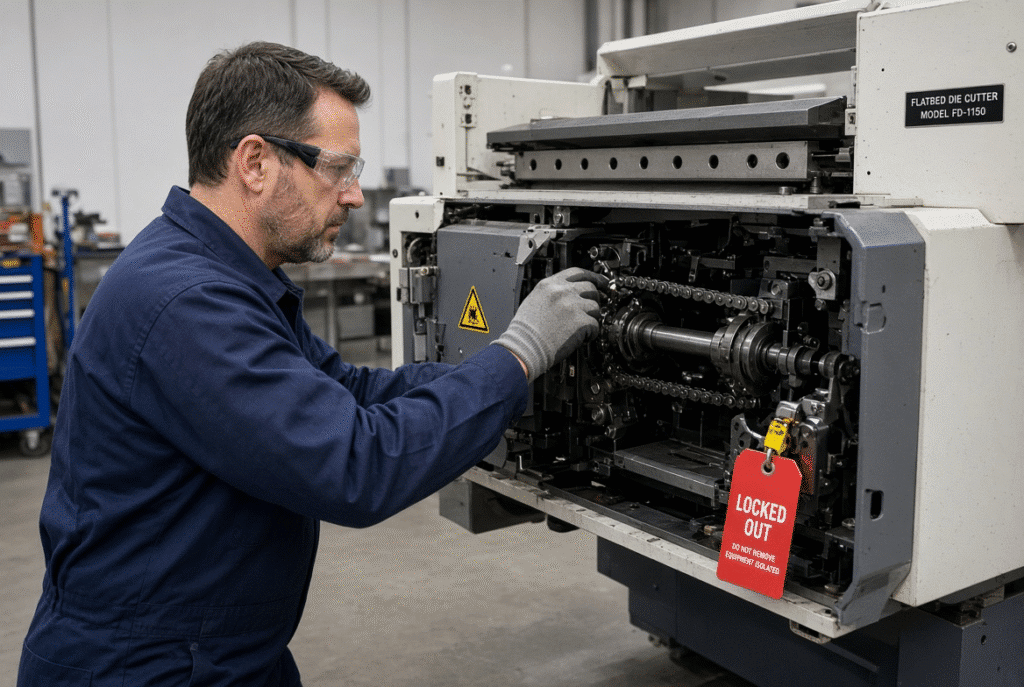
Board fibers, dried lubricant and scrap can get in guides, sensor and lubrication paths as well as paper dust. Follow the machine approved cleaning procedure and do not introduce any contaminants to the sealed bearings or guarded areas of the transmission. If you are using a guarded area, it should be kept closed as the machine is moving.
Lubrication and Oil Delivery
The lubrication method and interval is specified by the machine builder. Forced oil circulation, oil baths or grease points are used in some machines. The type of grade, oil level and freedom from contamination are of far greater importance than merely putting more oil in the system. Follow manufacturer’s instructions and machine’s own lubrication diagram.
Inspection of Bearings, Gears and Drive Interfaces
Qualified technicians look for wear marks, abnormal heat, noise, backlash, looseness and damaged contact surfaces. The intermittent mechanism should be evaluated with all of the related shafts, couplings, chains, sprockets and bearings. Different designs do not have a 100% clearance or 100% backlash limit.
Verify Timing After Service
When the timing relationship is disturbed by any work, which disturbs intermittent mechanism, chain system, gripper bars, and so on, and gears, change the timing relationship. Once served the approved timing marks or procedures must be checked by a qualified technician prior to the machine being returned to production. Critical timing is not adequate by visual approximation or operator trial and error.
Record Wear and Maintenance History
A trend picture is created from logging machine hours, observed symptoms, lubrication events, component replacements and registration complaint. With progressive wear, it’s usually easy to see the wear in the records before the production is halted by a sudden failure.
Diagnosing Sheet-Transfer Problems Systematically
When the problem isn’t intermittent, but is something else, the replacement of the intermittent mechanism will cost time and money. Begin at the lowest level of variables and proceed up to the transmission.
Check the Material and Sheet Condition
Even a good transport system can be compromised by curl, warp, moisture variation, thickness differences and damaged edges or poor pile preparation. Before deciding the mechanism is worn, check various batches and sheet types to see if there are any differences.
Check Feeding, Gauges and Sensors
Feeder timing, separation of sheets, front and side gauges, photoelectric sensors and limit switches all affect the position of the sheets. Determine if the error is at the sheet entry, during the transfer process or at the die or in delivery.
Check Gripper Bars, Chains and Sprockets
Symptoms from worn gripper teeth, elongated chain, damaged sprockets, guide wear or guide tension errors are identical to intermittent-drive symptoms. Check the complete transport process system.
Analyze the Symptom Pattern
If there is a consistent directional registration error, random scatter, speed related vibration or fault that only occurs every so often, they all lead to different causes. Document machine speed, material, job setup, defect(s) location and the specific stage of the cycle where the defect occurs.
How Intermittent Mechanisms Affect Production Speed and Output
Apart from feeding reliability, setup time, material behavior, inspection and downstream handling, stable cycle timing allows for predictable sheet transfer, but actual finished output depends on these factors as well.
Cycle Timing and Sheets per Hour
The sheets per hour rate is a theoretical maximum, as the intermittent mechanism controls sheets as they pass through each station. With set-up, pile changes, stops and rejects included real output is reduced.
Stability at Higher Operating Speeds
When mechanisms are worn or poorly adjusted, they usually make the operator slow down to prevent vibration or registration drift. A lower but consistent running speed will often produce more good sheets per shift without the high number of stops and scrap.
Downtime, Scrap and Maintenance Cost
Actually, it is the timing related jams, damaged sheets, emergency stop, secondary damage to chain/bearings etc that increase the actual cost per 1000 sheets. These are unnecessary costs that can be eliminated with preventive inspection and the proper lubrication.
What to Ask When Evaluating a Flatbed Die Cutter
The intermittent mechanism is not a black box, it’s a maintainable subsystem – buyers should treat it as such.
Questions About Mechanism Design
Describe the type of intermittent mechanism used, methods of controlling the timing in a sheet transfer, identify wear parts, methods of lubricating the mechanism, operating conditions tested, method of checking timing after operation, and maintenance documentation provided. Ask for precise technical answers, rather than vague statements of “high precision.”
Questions About Speed and Registration
Ask to try the material, sheet size, die layout, speed and registration during any demonstration or test. A low-speed trial with a basic sheet cannot be used to demonstrate performance in the buyer’s production environment.
Questions About Spare Parts and Service
Verify bearings, gears, chains, sprockets, lubrication parts, recommended service intervals, typical lead time and technician support. Long term value will depend on the plants ability to maintain the mechanism with clear procedures and availability of parts.
Intermittent Mechanism Considerations for the DAIS D1060
The DAIS D1060 automatic flatbed die cutter adopts high precision 240 degree intermittent mechanism to control the cycle of the die cutting part. Each cycle is also coordinated with the drive arrangement, which includes a wear-resistant worm gear and worm, crankshaft and transmission parts.
Sheet Transfer in a 1,060 mm Die Cutter
Controlling gripper movement and repeatable cycle timing is important for a machine handling up to 1060 x 770 mm to ensure the larger boards are not destabilized by the act of moving, dwelling and delivering. It is important to note that these figures of registration and speed performance still rely on material, tooling, set up and overall machine condition.
Maintenance and Lubrication Requirements
The following should be covered by the D1060 maintenance plan: the mechanism for intermittent; related transmission parts; forced lubrication system; gripper bars; chains and bearings. Information on intervals and lubricant specification is provided in the machine manual; these instructions override any general information.
Technical Review Before Ordering
Provide sheet size, board type, die layout, target speed and registration requirements when requesting a configuration review. This information enables the technical team to verify the machine and setup that has been selected is suitable for the desired production conditions.
Final Guidance: Timing Stability Is a System Responsibility
It is the intermittent mechanism that is the core of controlled sheet transfer and the effective die cutting timing is reliant on the entire system: feeder, gauges and sensors, gripper bars, chains, lubrication, transmission, tooling, material and maintenance discipline. Know the motion cycle, watch for early signs of trouble, use proper oil or grease, check all orifices connected to the clutch, timing after any service, and test the clutch at production conditions rather than top published speed.
Having sheet transfer instability, registration drift or excessive cycle noise? Provide DAIS with the model of the machine, material type, sheet size, operating speed and symptoms observed. We have a technical team to assist in identifying the information required for a sheet-transport or machine-configuration review.