

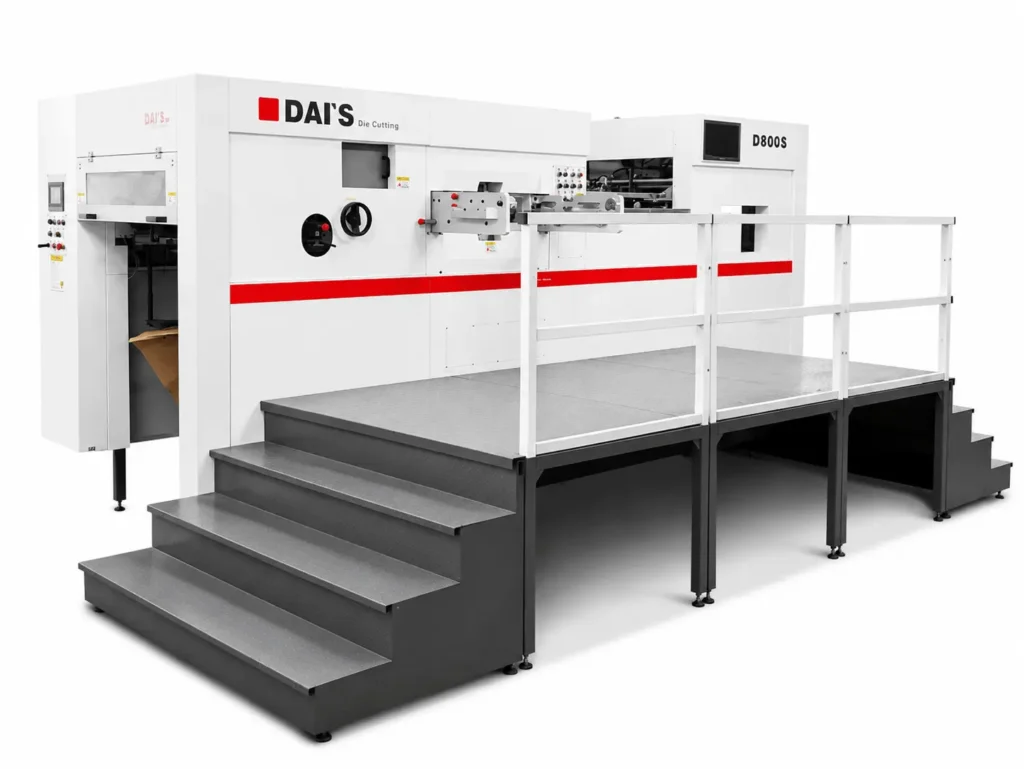
If manual platen pressing begins to restrict profitable production, a packaging plant should consider converting to a semi-automatic die cutter. Typical causes are increased labour demand for feeding and delivery, usable output that drops behind the printing line, inaccurate register and/or creasing, increased changeovers or delayed repeat orders. The speed of the rated machine is not always the key factor. This complete comparison includes sheet handling, saleable sheets, operator time, quality consistency, and the total cost per batch.
Manual platen press is still efficient for handling simple jobs, short runs, and samples. The same process is often the choke point in the converting chain when volume, product complexity or delivery pressure increases.
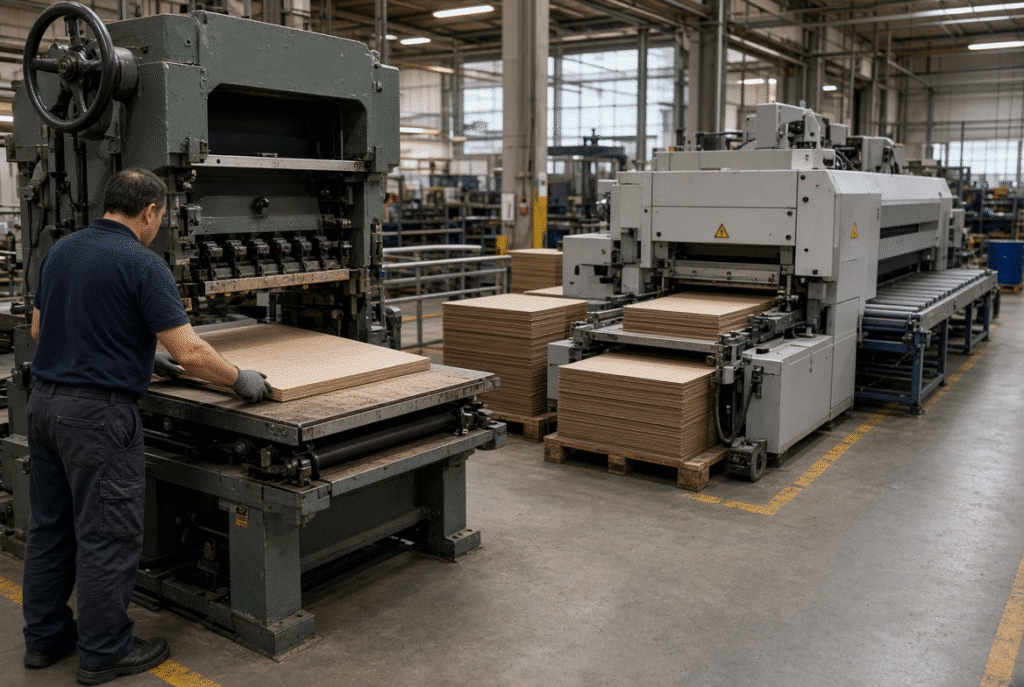
What Is the Difference Between a Manual Platen Press and a Semi-Automatic Die Cutter?
Manual platen press is highly dependent on the operator in almost every operation involved in the handling of the sheet. A semi-automatic flatbed die cutter is mechanically controlled for feeding, registration and delivery, but still requires an operator to prepare piles, supervise and change dies.
Manual Platen Press Workflow
The operator sets up the pile, slides or lifts each sheet into the press, closes the press, removes cut sheet and piles or checks sheet. Each sheet has to go through the hands of the operator. Speed and consistency are influenced by fatigue, slight variations in placement and the time it requires to remove waste or reset the sheet. This process is still usable for very small quantities of products and unusual specialty tasks.
Semi-Automatic Die Cutter Workflow
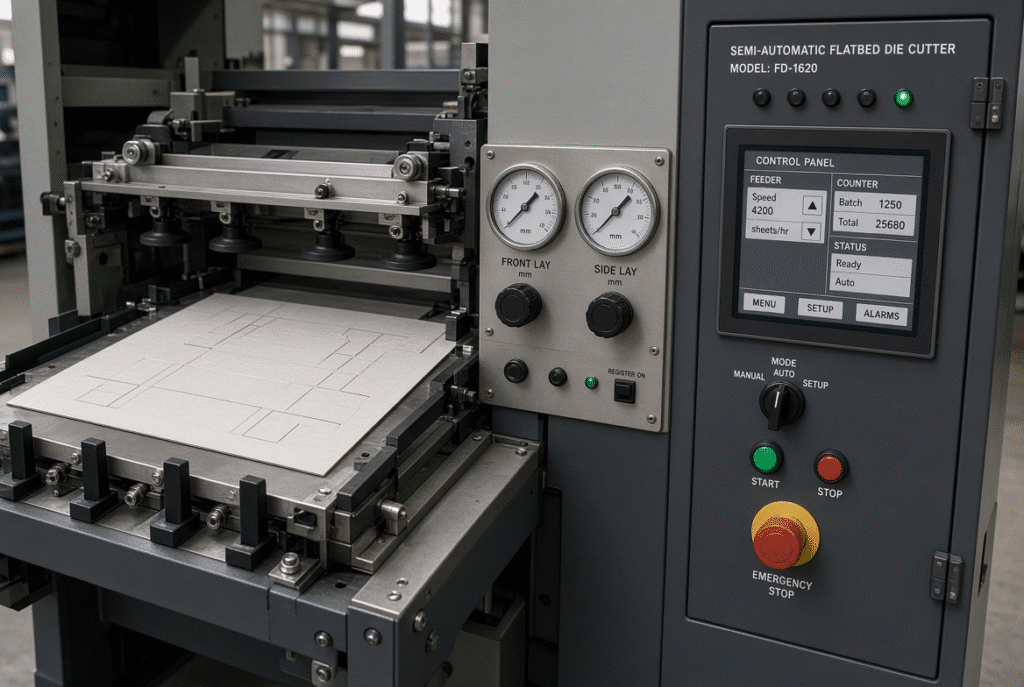
A semi-automatic machine will normally employ a feeder or controlled transport system to feed the sheet, front and side gauges for registration, a mechanical platen for pressure and a delivery section to stack the finished sheets. The operator continues to load the pile, monitor the run, change over and inspect output but continuous hand placement and lifting of individual sheets is decreased. The degree of automation varies with each model; see the actual model.
Why the Category Name Is Not Enough
There are various differences between two semi-automatic machines, one in sheet size range, another is maximum pressure, another is feeding method, another is delivery height, another is the type of safety guards included and others are the options available in the machine. The technical specification is the one to compare. Ask for the full list of set-up requirements and, if possible, a production test using the plant’s own dies and materials.
Where Manual Platen Presses Still Make Sense
Equipment is not ‘obsolete’ if it’s manual. It’s a sensible decision in the appropriate production context.
Low-Volume and Irregular Production
The manual press may be more cost-effective, based on the lower capital investment, if orders are not regular, batch sizes are small or demand is difficult to predict, and the number of sheets to be processed is limited. Don’t assume that the purchase price is the best indicator of the labor and handling cost.
Simple Products and Flexible Job Mix
Manual handling is preferred for simple die layouts that have low internal waste and high product change frequency. When the equipment is short-run oriented, like specialty paper items and/or highly varied customer orders, the make-ready can be structured or not.
Limited Capital or Early-Stage Production
If you are growing a new plant or launching a new business and need to prove out the market, you can begin with a manual press. The issue is to set the volume, labour or quality level up front which will justify an upgrade; planning rather than reaction.
The Main Operational Differences Between the Two Systems
Practical comparison is focussed on labour, finished output, quality consistency, changeover behaviour and safety.
| Factor | Manual Platen Press | Semi-Automatic Die Cutter |
| Labor focus | Continuous sheet feeding, positioning, delivery | Pile prep, supervision, inspection, changeovers |
| Typical usable output | Limited by operator pace and fatigue | More stable running speed, still material-dependent |
| Registration consistency | Operator technique dependent | Mechanical gauges and transport assist |
| Changeover style | Highly flexible for one-offs | Structured setup, better for repeat runs |
| Ergonomic load | High repetitive lifting and reaching | Reduced continuous handling |
Labor Requirements and Operator Workload
A manual press often needs continuous attention from one or more operators for feeding and delivery. Semi-automatic systems shift effort toward preparing the pile, watching the run, and performing inspections. Labor is not eliminated; it is reallocated to higher-value tasks.
Production Speed and Finished Output
Usually, a manual press requires constant attention by either one or more operators for feeding and delivery. Semi-automatic systems will free up manpower and allocate resources to load preparation, run supervision, and inspections. Labour is not removed, it is shifted to more productive activities.
Registration and Cut Quality
Rarely, catalogue speed figures will be the same as completed saleable sheets. Less net output due to manual feeding, pile changes, fatigue, and inspection. With a semi-automatic machine, the speed of the run is more consistent but the actual speed is still dependent upon material type, die complexity and stoppages. Look at saleable sheets per shift and not theoretical maximum.
Changeover and Job Flexibility
Manual presses are flexible and change easily for one-off or odd jobs. Typically, semi-automatic machines need a more formal make-ready procedure that works best in situations where the same die is used repeatedly or when the volume makes up the expense of the make-ready.
Safety and Ergonomics
A manual press causes repetitive exposure due to sub-optimal feeding patterns, poor positioning and close proximity to moving parts. Most modern semi automatic machines will have the standard safety features: guards, photoelectric protection and emergency-stop buttons. Even if the equipment is safe, it requires training, maintenance and proper application of safety equipment.
Warning Signs That a Manual Press Is Limiting the Plant
It is these signals that are meaningful when they occur regularly and not just in one very busy period.
Labor Cost Is Growing Faster Than Output
Monitor manual die-cutting area operators, overtime hours, training time and rework. If the price of labor per finished batch increases at a greater rate than the number of batches, the economics of that workflow need to be examined.
Die-Cutting Output Falls Behind Printing
A measurable bottleneck occurs if the printing or laminating department always generates work in process (WIP) that is not able to be picked up by the die-cutting section. Make a comparison of the actual finished sheet from the entire production chain.
Orders Are Delayed by Feeding and Delivery
Frequent sheet moves, patching, or ongoing “babysitting” of the press is a sign that the workflow is now not as robust as it needs to be when moving to a new sheet, patching, or “babysitting” the press.
Quality and Rework Are Increasing
Registration inconsistencies, incomplete cuts, creasing that is not even or edges that are damaged can indicate process strain. Check for the root cause (tooling, material, maintenance or machine limitations) before pointing at the press as the culprit.
Operators Are Regularly Working Around the Process
Constant repositioning of sheets, temporary fixes, or continuous “babysitting” of the press signal that the current workflow is no longer robust enough for the load it carries.
How to Evaluate the Upgrade Financially
Collect plant-specific numbers rather than relying on generic payback claims.
Calculate the Current Cost of Manual Production
Include operators and shifts, wage and overtime rates, average finished output, changeover time, waste and rework, delayed-order costs, maintenance, material handling, and supervision. Express the total as cost per finished batch or per 1,000 saleable sheets.
Estimate the Full Semi-Automatic Investment
Add the machine price, tooling, shipping, installation, commissioning, training, any floor or electrical preparation, spare parts, and initial service. A machine-only quotation understates the true cost of making the equipment operational.
Compare Usable Output and Labor Reassignment
Focus on finished saleable sheets, not catalogue speed. Consider whether the same team can handle higher volume or whether operators can be reassigned to inspection, packing, or another machine. Headcount reduction is not automatic; higher utilization of existing labor is often the larger gain.
Consider Utilization and Future Growth
A semi-automatic machine delivers value when it runs consistently across jobs and shifts. Use conservative monthly volume estimates that reflect actual customer demand, seasonal patterns, and realistic growth rather than peak theoretical capacity.
Production and Product Factors That Affect the Upgrade Decision
Machine format and automation level must match the products the plant actually runs.
Sheet Size and Material Range
Confirm maximum and minimum sheet size, maximum die-cutting area, board thickness, and material type with representative samples. White board, folding carton stock, and corrugated board behave differently; treat them as separate categories.
Die Layout and Product Complexity
Dense layouts, small waste pieces, intricate creasing, or tight registration requirements may need better pressure control and sheet transport than a manual press can reliably deliver, even if volume is moderate.
Batch Size and Order Frequency
Long repeat runs favor more automation. Frequent short runs place higher value on flexibility and quick changeover. Compare the complete job cycle from die installation through trial sheets, production, inspection, and cleanup.
Required Output and Delivery Schedule
Calculate the finished sheets needed to meet customer demand across available shifts and working days. Size the machine for realistic volume plus measured growth, not for a single peak day or for today’s average alone.
What to Evaluate in a Semi-Automatic Die Cutter
Consider the machine as a total feeding, cutting, control and delivery system.
Sheet Feeding and Registration
Check for controlled sheet separation, front and side gauges, gripper transport and ease of registration adjustment. Try the system with the plant’s actual materials such as any warped, coated or heavier sheets that are a frequent occurrence.
Pressure, Frame and Mechanical Stability
Both the quality of the cuts and the repeatability of cuts are influenced by working pressure, platen rigidity, and transmission design. In the case of the DAIS D1060 machine, for example, sheet size is limited to 1060 × 770 mm, die-cutting area is 1050 × 760 mm and the maximum working pressure is 300 tons. Check each figure from the exact quotation and trial results.
Delivery and Pile Management
The delivery-table lifting, paper leveling and pile-height capacity minimize the manual task of collecting and aligning completed paper. Cleaner stacks for next process with better delivery control.
Safety and Operator Controls
Visually assess guards, emergency stops, photoelectric protection, control interface clarity and access procedures. Ensuring safety relies on installing, maintaining and using safety features properly.
Maintenance and Service Support
Inquire as to lubrication points, wear parts, availability of spare parts, training, warranties, and service response time. The support terms are as important as mechanical specification, and a semi-automatic die cutter is a multi-year production asset.
When a Semi-Automatic Upgrade May Not Be the Best First Step
It is not always a question of new equipment.
The Real Problem Is Tooling or Make-Ready
Many of the common problems of incomplete cuts, poor creasing or slow setups can be traced back to die condition, make-ready technique, or pressure adjustment. Check tooling records and setup procedures, and then decide that the press doesn’t need to be replaced.
The Bottleneck Is After Die Cutting
If manual waste stripping, inspection, folding or gluing cannot accommodate more material to be processed in the finished state, then a quicker die cutter just pushes the pile of unfinished material downstream. Find the diagnosis for the whole line.
Production Volume Does Not Support the Investment
If the machine is not being used much, if the orders are not regular, or if the demand is still being validated in the system, then it can be a challenge to make the semi-automatic machine worthwhile. Work around process changes, improved scheduling or temporary subcontracting may be more appropriate temporary solutions.
A Practical Upgrade Decision Checklist
Record Current Production Data
Track the number of finished sheets per hour, operators working, actual running time, setup and changeover time, downtime, rework and waste, order delays, product mix, average and peak monthly volume, and labor and overtime cost. Numbers trumps assumptions based on catalogue speed.
Define the Required Machine Configuration
Record maximum and minimum sheet size, maximum die cutting size, material thickness range and feeding and delivery requirements, stripping requirements, electrical standard, installation requirements, training and service requirements. This list allows you to make supplier quotations that are comparable.
Request a Sample Trial or Technical Review
Give actual board layouts, product layouts, die specifications, and production specifications. A good trial tests the feeding system, registration, cutting, delivery, changeover and output in realistic conditions. Request references from plants that are producing similar packaging products.
Final Guidance: Upgrade When the Workflow, Not Just the Press, Requires It
Manual platen presses are still very much suited for low volume production, flexibility and simplicity. The semi-automatic die cutters are the superior commercial solution whenever lab hours, throughput, quality uniformity, safety exposure, or customer delivery pressure are measurable factors limiting the overall converting process. It should be based on how the entire production system works, and not just on the specification of a particular machine, that is, from printing to die cutting, waste removal, inspection, and packing.
Thinking about upgrading the manual platen press? Submit your sheet size, board type, product layout, current output and your operator requirements and destination to DAIS. We can review if a semi-automatic product like the D1060 works for your production model.